
Univar, Middlesbrough: Dry Cooler Replacement & Process Cooling Support
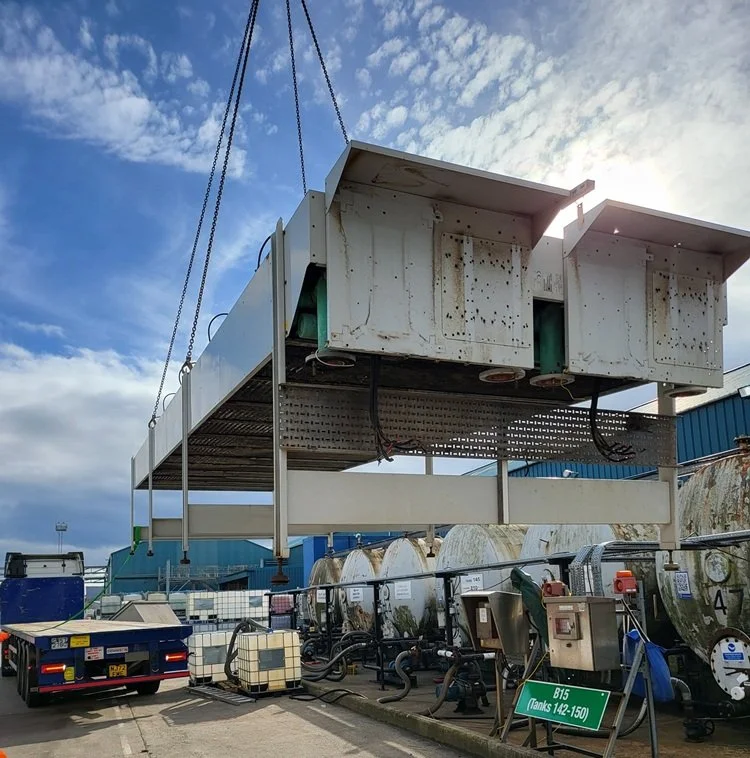
Removal of the existing corroded dry air cooler at Univar’s Middlesbrough site. Cooltech Products supported the replacement project with a site survey, cooling-capacity review, equipment selection, installation assistance and on-site commissioning.
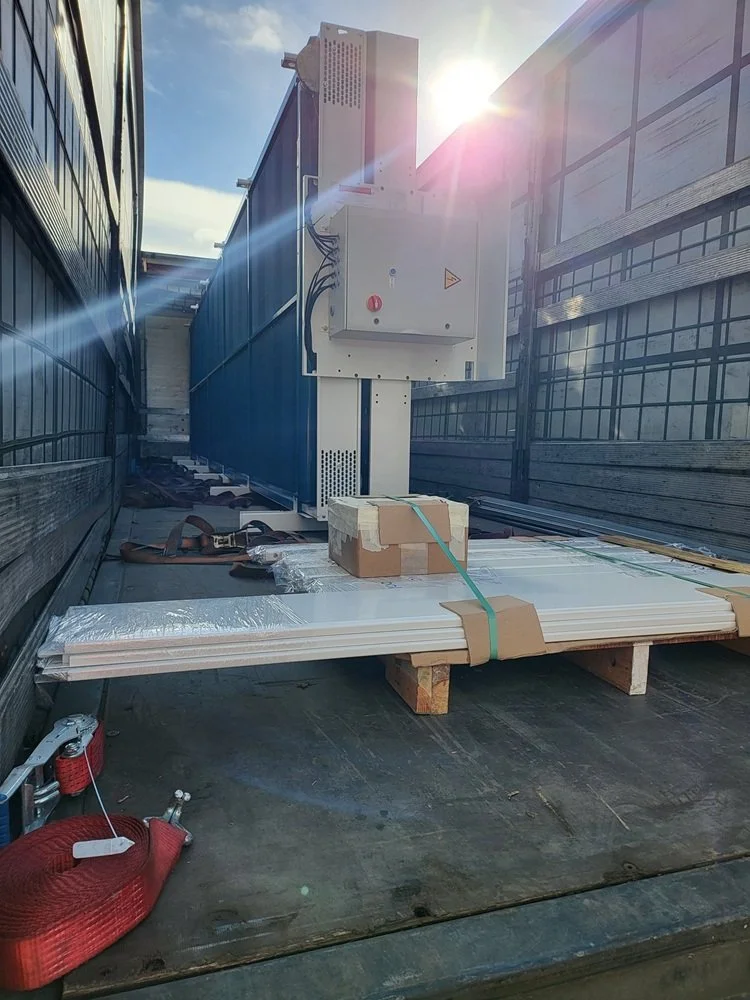
The replacement dry air cooler loaded for delivery to Univar’s Middlesbrough site. Specified by Cooltech Products, the unit incorporates AquaAero corrosion protection, EC fans and a dedicated control panel to support the site’s process-cooling requirements.
Site assessment, interim maintenance and a 515 kW dry cooler replacement
Project at a glance
Application: Cooling supporting a sulphuric-acid dilution process
Challenge: Severe corrosion of the existing dry cooler in a chemically aggressive atmosphere
Selected duty: 515 kW at 18°C entering air, cooling 30% ethylene glycol from 28°C to 23°C
Cooltech support: Site survey, capacity review, chemical-compatibility assessment, P&ID support, installation assistance and on-site commissioning
The figures above are equipment selection conditions, rather than measured commissioning results.
The challenge: cooling performance was affecting production
Cooltech Products surveyed an existing dry air cooler at Univar’s Middlesbrough site following severe deterioration of its copper-tube, aluminium-fin heat exchanger.
The site assessment identified atmospheric exposure to hydrochloric and sulphuric acids as a key factor in the corrosion. Aluminium fins had become brittle and deteriorated away from the copper tubes, leaving substantial areas of the coil ineffective.
This had consequences beyond equipment condition. Sulphuric-acid dilution releases heat, which must be removed during processing. Reduced cooling capability was extending batch processing times and constraining production throughput.
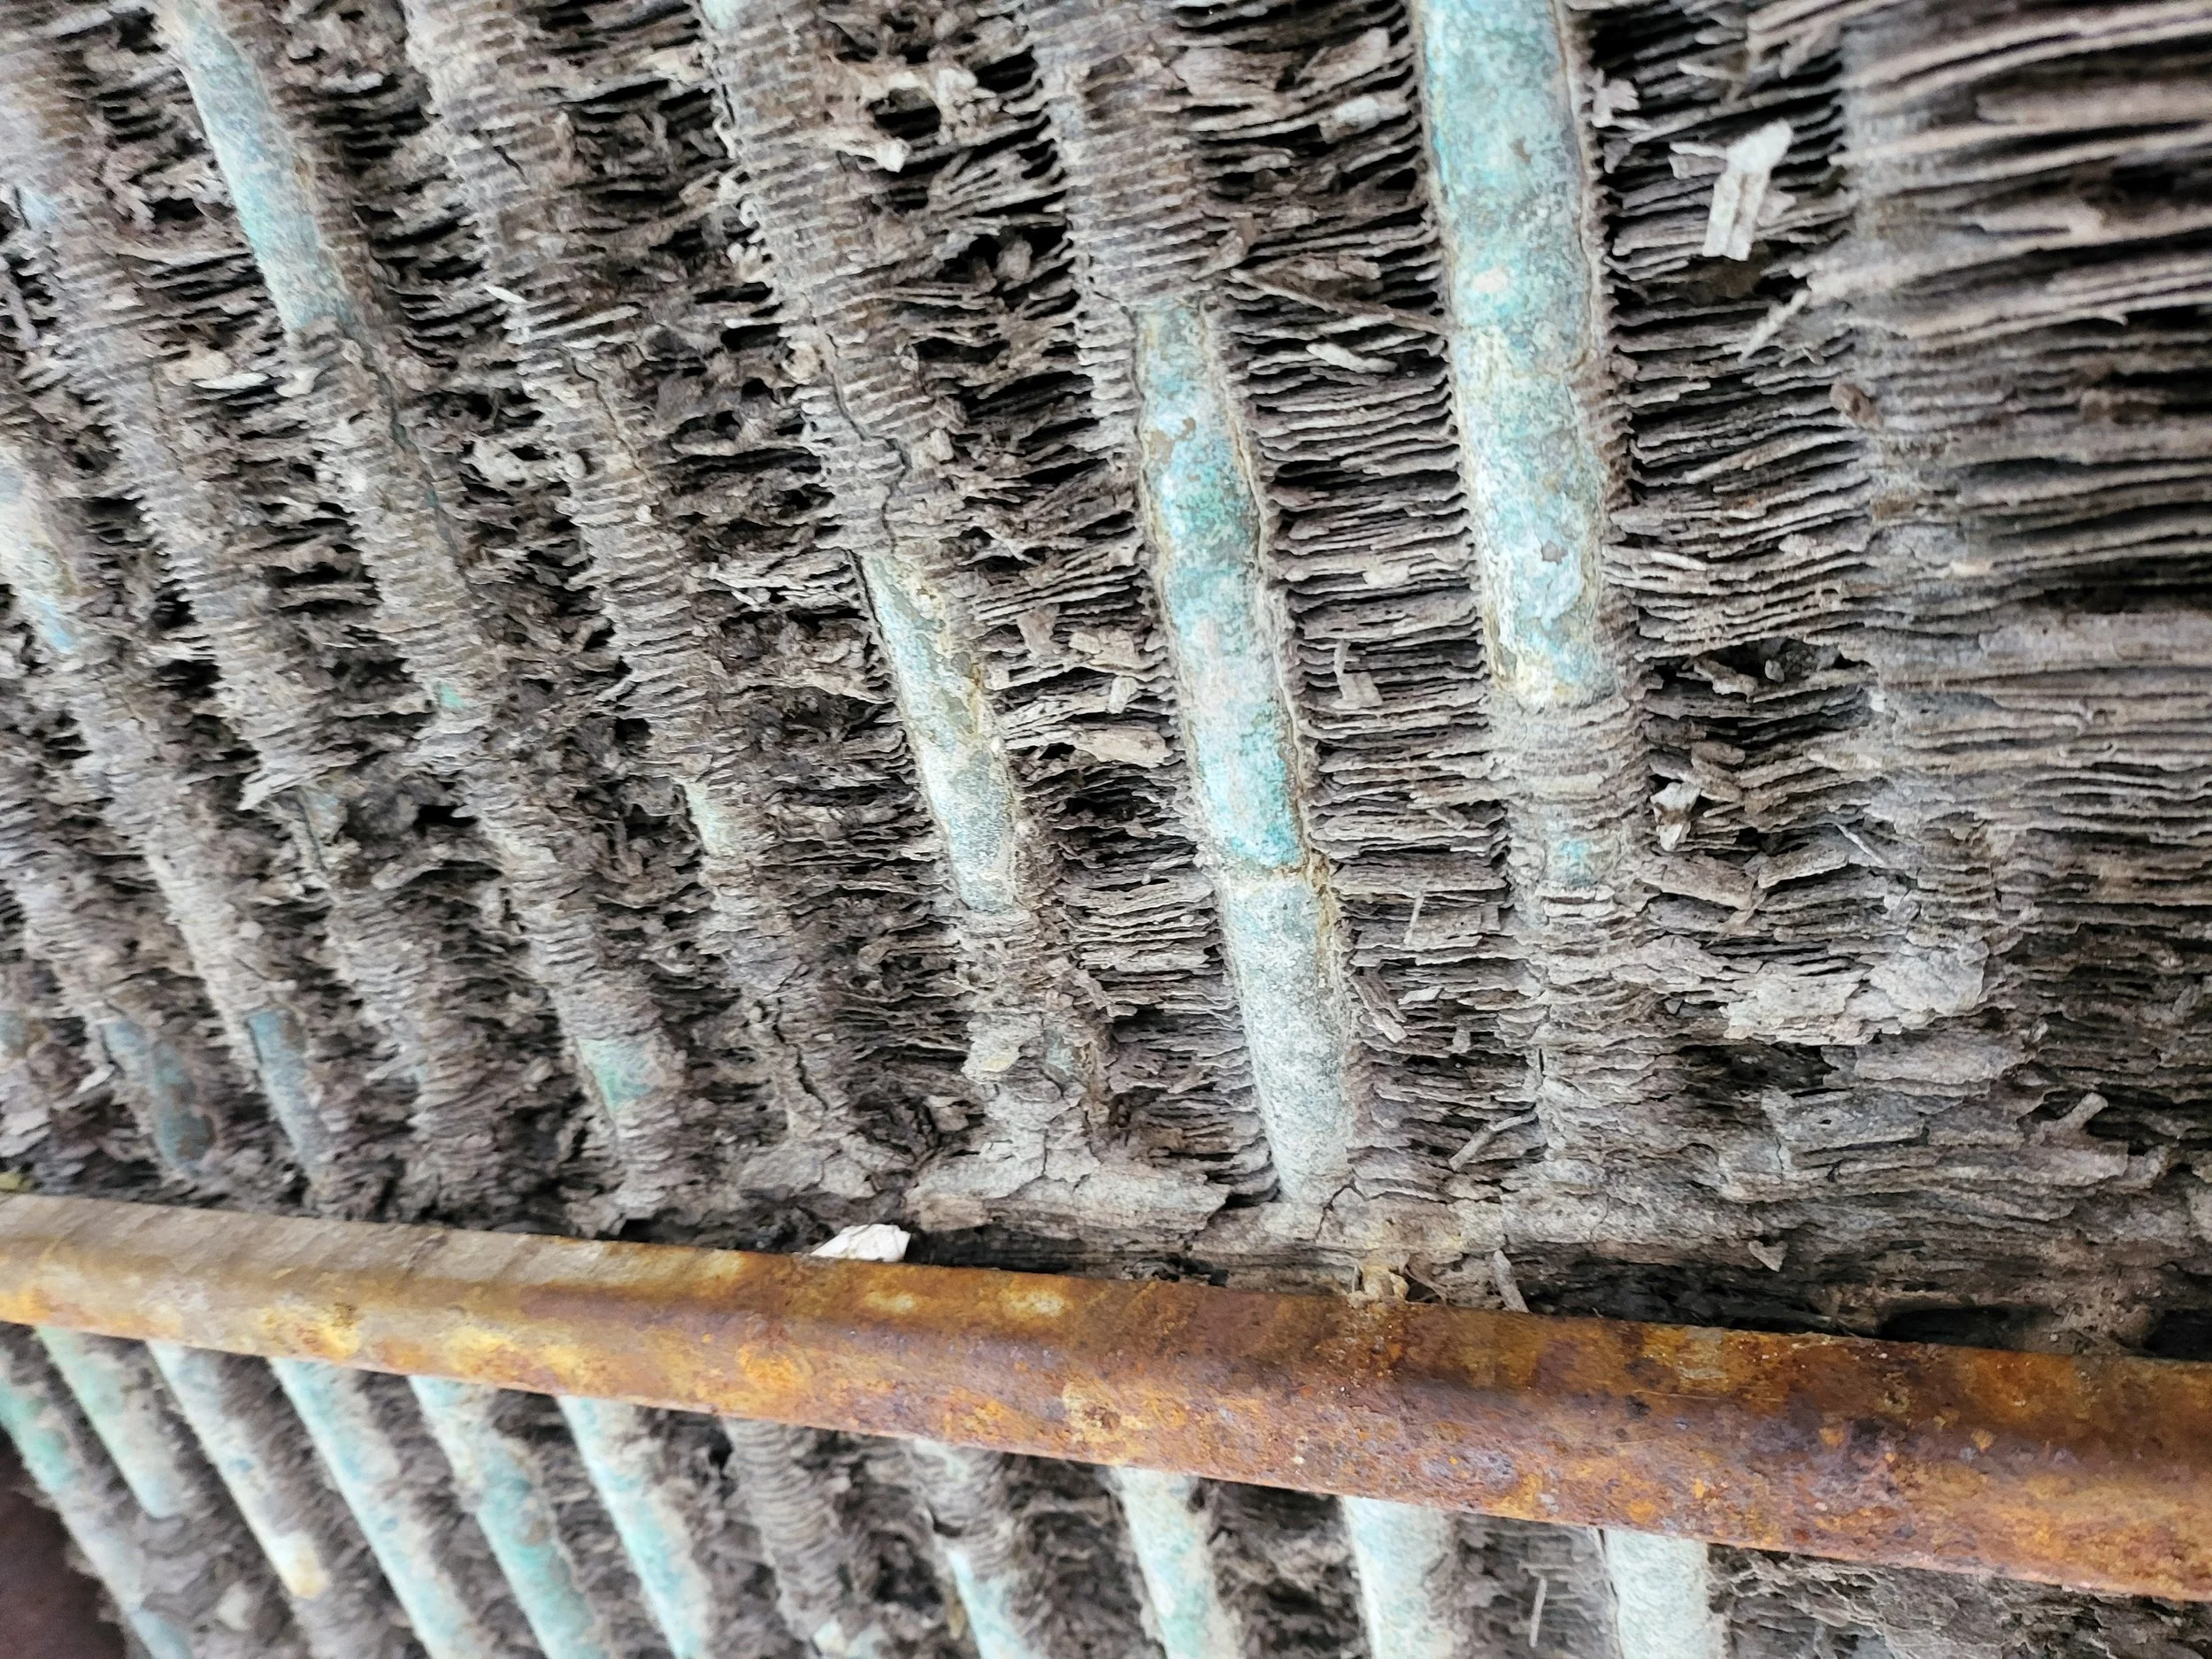
Corrosion
Severe corrosion of the existing dry cooler’s aluminium fins, with sections deteriorating away to expose the copper tubes. The loss of effective fin surface and accumulated deposits reduced heat-transfer performance, contributing to the cooling constraints affecting Univar’s production process.
Immediate support: improving the remaining cooling performance
Before replacement, Cooltech carried out a specialist deep clean using hot water with the fans stopped, improving the performance of the remaining heat-transfer surface.
Cooltech has developed cleaning and restoration methods designed to minimise further damage to already corroded fins. This involves more than pressure washing with a coil cleaner: our approach considers the condition of the coil, the effects of corrosion on fin integrity and thermal contact, and how accumulated deposits restrict airflow and heat transfer.
Although cleaning cannot replace lost fin material or reverse corrosion damage, a carefully assessed deep clean can recover useful cooling performance and help slow further deterioration. Where production is constrained by cooling capacity, even a modest improvement can make a practical difference.
At Univar, the clean improved cooling sufficiently to increase production throughput, providing an interim benefit while the replacement solution was being prepared.
Engineering the replacement
Cooltech reviewed the process cooling requirement to assess whether replacement capacity should increase, decrease or remain comparable, rather than simply replicating the existing equipment.
The selected dry cooler was rated at 515 kW, with ten EC fans, at the stated design conditions.[1]
Corrosion protection was a central consideration. Cooltech assessed chemical compatibility and recommended an AquaAero CX coating option, taking account of the application and the size of the equipment.[1]
Supporting Aqua Aero documentation includes independent accelerated-corrosion testing. One report records no visible defects on coated aluminium panels after 20,000 hours of neutral salt-spray exposure.[2] These laboratory results provide supporting evidence of coating performance, rather than a prediction of service life or proof of resistance to every chemical exposure.
Support through installation and commissioning
Cooltech’s involvement extended beyond equipment selection and supply:
Piping and instrumentation diagram support.
Process advice and review of cooling capacity.
Chemical-compatibility assessment.
Assistance with installation.
On-site commissioning.
This brought the equipment selection and practical site requirements together, with technical support continuing through to commissioning.
Maintaining performance over time
The project highlights the relationship between heat-exchanger condition and production capability. Suitable corrosion protection and a planned maintenance regime both form part of the long-term cooling strategy.
Aqua Aero’s general conditions provide for up to ten years of limited coating warranty, subject to applicable exposure limits, maintenance and other conditions. This is coating cover, not a complete-unit or replacement-coil warranty.[3]
Have a cooling system affected by corrosion, reduced performance or changing process requirements?
Cooltech Products can assist with site assessment, thermal selection, replacement planning and commissioning support.
References
[1] Equipment selection sheet, 27 October 2025; reference 210142EB-R / Order 1013; model DR90D525(170)-10V SSFL AQA SIL ISS WEPF 1.
[2] COT laboratory report LAB21-0188-REP: Aqua Aero Coil Coating II, 20,000-hour ASTM B117 neutral salt-spray exposure.
[3] Aqua Aero General Warranty Conditions, version 032025.1.
Project observations and service outcomes supplied by Cooltech Products.